Choosing the best Ceramic Insulated Band Heater in China requires more than comparing prices, wattage, or stainless-steel finishes. A reliable selection must match the barrel diameter, operating temperature, heating zone, insulation quality, and production rhythm. In a busy plastics workshop, the heater should transfer heat evenly, recover quickly, and avoid creating cold bands near the nozzle. Small design details matter.
Industrial heating engineer David A. Moore explains, “A band heater performs well only when its heat reaches the process evenly.” This principle deserves attention. A powerful heater is not automatically an efficient one. Poor contact, uneven clamping, or inaccurate temperature sensing can waste energy and shorten service life. The best supplier should provide clear technical data, stable resistance values, inspection records, and practical installation guidance.
Experience also exposes uncomfortable weaknesses. Some products look polished but deliver inconsistent heating after repeated thermal cycles. Others meet a catalogue specification yet fail in real production. That gap matters. Buyers should examine ceramic density, mica or mineral insulation, terminal strength, surface temperature, and quality-control procedures. Ask for test evidence, not attractive promises.
China offers many capable Ceramic Insulated Band Heater manufacturers, but quality varies between factories. The strongest candidates understand both electrical design and actual molding-machine conditions. They communicate tolerances clearly. They also admit limits when a custom design is necessary. This guide will compare heater construction, performance, safety, customization, supplier credibility, and long-term value. The answer may not be the cheapest option. It may be the heater that remains stable when production becomes demanding.
What Is the Best Ceramic Insulated Band Heater in China?
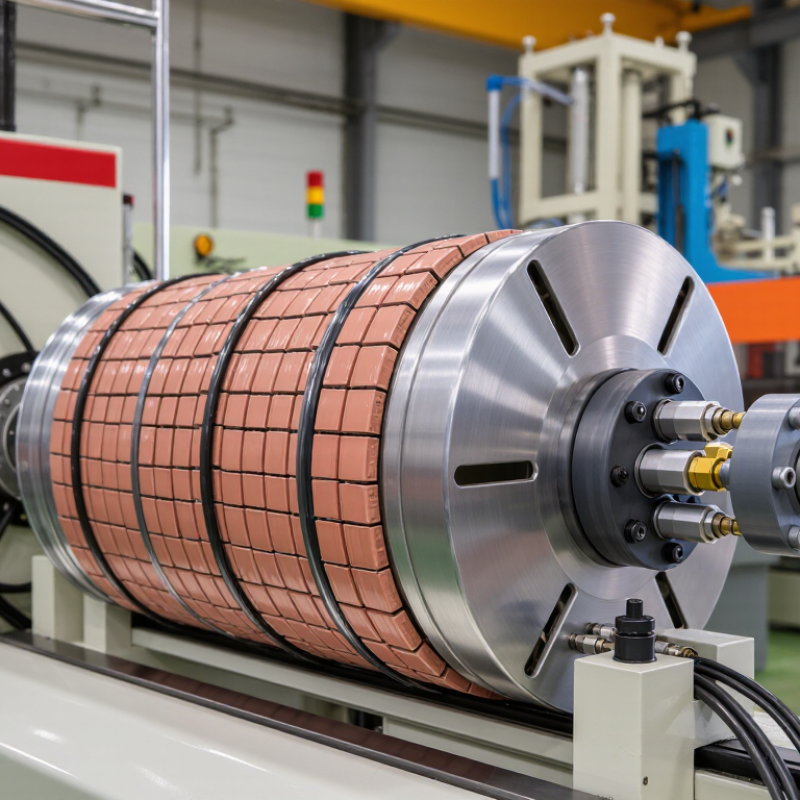
A ceramic insulated band heater is an electric heating device wrapped around a cylindrical surface. Its core contains resistance wire embedded in ceramic blocks. These blocks transfer heat toward the barrel while reducing heat loss to the outside. A metal sheath then protects the assembly from vibration, moisture, and daily handling.
In practical equipment checks, the heater should fit the barrel closely. Even a small gap can create hot spots and slow heat transfer. Ceramic insulation also helps the heater reach higher operating temperatures than many simple metal heaters. It is commonly used on injection molding machines, extruders, pipes, and processing cylinders. The best specification depends on diameter, width, voltage, wattage, temperature range, and required heating speed.
Check the wiring carefully. Poor terminal connections may cause resistance heating in the wrong place. Surface temperature should be measured during a trial run, not guessed from the controller display. I have seen heaters selected only by size, then replaced because their wattage was too low. That mistake is avoidable, but catalog figures can still mislead. Ceramic elements may crack after severe impact or uneven tightening. Gentle installation matters. So does confirming insulation resistance before operation. A reliable supplier should provide test data, material details, dimensional tolerances, and clear installation guidance. No heater is perfect. The working conditions decide whether a ceramic insulated band heater performs well.
Ceramic insulated band heaters are commonly selected for high-temperature plastic processing, nozzles, dies, and barrels. Typical ceramic constructions can operate at approximately 760°C, offering a higher temperature capability than many mica-insulated designs. Actual performance depends on heater construction, watt density, clamping, temperature control, and application conditions.
A ceramic band heater works by turning electrical resistance into controlled heat around a cylindrical surface. Inside the heater, resistance wire carries current and produces Joule heat. Ceramic blocks or fiber insulation hold the wire in place and reduce heat escaping outward. The heat then moves through the metal sheath by conduction, warming a barrel, nozzle, pipe, or mold.
A thermocouple measures surface temperature, while a controller adjusts electrical power in short cycles. Good contact matters. A loose band can create cold spots, longer heating times, and damaged wiring. The U.S. Department of Energy’s 2022 Industrial Decarbonization Roadmap reports that process heating uses about 51% of manufacturing energy. Better heat transfer can therefore reduce wasted electricity, although heater efficiency alone cannot fix poor insulation or incorrect settings.
Ceramic insulation also supports higher operating temperatures than many basic band-heater designs. In practical testing, technicians should check clamping pressure, barrel cleanliness, and sensor placement before increasing wattage. That small inspection is often overlooked. Ceramic heaters are not automatically the best choice. Excessive power density may overheat a thin metal surface, while weak insulation can still waste energy. Performance depends on diameter, width, voltage, temperature range, and the material being heated. Reported laboratory values may not match a dusty production line. That is where careful measurement matters.
The best ceramic insulated band heater combines stable heat, strong insulation, and precise construction. In field service, uniform temperature matters more than impressive wattage. A well-designed ceramic core reduces heat loss around plastic barrels, nozzles, and dies. It also supports higher operating temperatures than many basic band heaters. Check the heater’s temperature range, watt density, and voltage before ordering. These details must match the machine, not just the product photograph.
Mechanical fit is equally important. The band should wrap evenly without gaps or forced bending. Stainless steel sheaths resist moisture and repeated installation, while reliable terminals reduce loose-connection risks. Ask for resistance testing, insulation testing, and dimensional inspection records. Traceable production documents can reveal whether quality is consistent across batches. However, testing alone is not enough. I have seen technically correct heaters fail after poor clamping and uneven contact.
Tips: Measure the barrel diameter when cold. Confirm the thermocouple position. Request a sample before bulk production. Compare actual temperature readings during a trial run. Leave room for adjustment; real machines are rarely perfect. Ceramic heaters can be efficient, but careless installation still creates cold spots, overheating, or cracked insulation. A dependable supplier should explain these limitations clearly and provide practical installation guidance.
Choosing the best ceramic insulated band heater in China starts with comparing manufacturers, not catalog photos. A reliable supplier should explain ceramic composition, insulation thickness, watt density, and operating temperature. These details affect heating speed, energy use, and service life.
During practical equipment evaluations, I check whether the manufacturer provides clear drawings and stable test records. Ask for resistance tolerance, insulation resistance, dielectric strength, and temperature uniformity data. A serious factory should offer samples before large orders. It should also identify heating wire materials and terminal construction. Traceable batch numbers matter when a heater fails months later. Some suppliers provide impressive specifications but weak documentation. That gap deserves attention.
Tips: Compare at least three factories using the same technical sheet. Inspect ceramic density and surface finish on sample units. Request photographs of winding, wiring, and final testing. Confirm the actual clamping diameter, band width, voltage, and power. Ask how defects are handled, including replacement time and inspection responsibility. Do not judge only by the lowest quotation. A cheaper heater may use uneven winding or thinner insulation. I have seen small dimensional errors create loose contact and slow heating. Still, inspection is not perfect; incoming checks can miss failures under vibration or repeated thermal cycling. Require a trial run whenever the application is critical.
The best ceramic insulated band heater is determined by application requirements rather than price alone. Use the following objective comparison criteria to evaluate Chinese manufacturers, request supporting documentation, and select the supplier with the strongest technical fit.
| Comparison Dimension | Recommended Benchmark or Typical Technical Data | Why It Matters | Information to Request from the Manufacturer | Priority |
|---|---|---|---|---|
| Heating Temperature | Typical continuous operating range: approximately 300–700°C, depending on construction, insulation, power density, and application. | The heater must safely reach the required process temperature without premature insulation or sheath degradation. | Rated operating temperature, maximum surface temperature, thermal test report, and application-specific temperature curve. | High |
| Insulation Material | Ceramic fiber, ceramic beads, or ceramic modules with high-temperature electrical insulation. | The insulation system affects heat resistance, dielectric safety, mechanical stability, and service life. | Material specification, insulation structure drawing, supplier data sheet, and high-temperature aging information. | High |
| Watt Density | Common design range: approximately 3–8 W/cm²; the correct value depends on barrel material, temperature, airflow, and heating cycle. | Excessive watt density can create hot spots, while insufficient watt density may cause slow heating and poor process control. | Calculated watt density, heated-area calculation, load diagram, and recommendations for the specific machine. | High |
| Voltage and Power Accuracy | Available for common industrial supplies such as 110 V, 220–240 V, and 380 V; confirm resistance and rated power against the requested voltage. | Incorrect resistance or power can cause overheating, slow warm-up, unstable temperature control, or circuit overload. | Nameplate data, resistance value at room temperature, power tolerance, wiring diagram, and inspection record. | High |
| Electrical Insulation Resistance | A high-temperature heater should be supplied with a documented insulation-resistance value measured at the specified test voltage. | Good insulation resistance reduces leakage-current risk and supports safe operation around operators and control equipment. | 100% insulation-resistance test record, test voltage, test temperature, acceptance limit, and test equipment calibration status. | High |
| Dielectric Strength | The supplier should define a dielectric withstand test suitable for the heater voltage and insulation design. | The test helps identify insulation breakdown that may not be detected by a simple resistance measurement. | Hi-pot test voltage, test duration, leakage-current limit, pass/fail standard, and batch test report. | High |
| Temperature Uniformity | Uniformity should be specified for the actual heated length and measured under defined installation conditions; zoning may be required for long barrels. | Uneven heating can cause material degradation, inconsistent molding, poor extrusion quality, and localized barrel wear. | Thermocouple layout, thermal imaging or temperature-mapping report, zone design, and test conditions. | High |
| Dimensional Fit | Confirm internal diameter, heater width, heated length, clearance, clamping method, terminal position, and allowable expansion. | A poor fit can reduce heat transfer, create mechanical stress, or leave unheated gaps on the barrel. | Dimensioned drawing, CAD file, installation photos, tolerance table, and approval sample before mass production. | High |
| Mechanical Construction | Rigid ceramic modules or flexible ceramic-insulated construction should match the machine's vibration, clamping, and maintenance requirements. | The structure must withstand installation and repeated thermal expansion without cracking or loosening. | Cross-sectional drawing, fastening method, terminal protection details, vibration considerations, and sample inspection. | Medium |
| Thermal Expansion Compensation | The design should include suitable clamping clearance, spring-loaded fastening, or other compensation for thermal expansion. | Correct compensation maintains contact with the barrel and lowers the risk of deformation or hot spots. | Installation instructions, recommended tightening method, expansion allowance, and maintenance procedure. | High |
| Lead Wires and Terminals | Lead insulation, terminal hardware, length, orientation, and temperature rating must match the installation environment. | Terminals and wires are frequent failure points when exposed to heat, vibration, contamination, or incorrect routing. | Wire and terminal specifications, temperature rating, wiring diagram, strain-relief design, and terminal torque requirements. | High |
| Quality-Control Process | Key controls should include resistance, power, dimensions, insulation resistance, dielectric strength, visual inspection, and packaging inspection. | A documented process reduces batch variation and makes product failures traceable. | Inspection and test plan, sample quality record, lot traceability method, nonconformance procedure, and calibration certificates. | High |
| Material Traceability | Heating wire, ceramic insulation, terminals, lead wires, and metal components should be identifiable by batch or purchase record. | Traceability supports root-cause analysis and consistent repeat orders. | Material certificates where applicable, batch numbers, incoming inspection records, and production records. | Medium |
| Customization Capability | The supplier should support custom diameter, width, wattage, voltage, thermocouple openings, zones, terminals, and mounting arrangements. | Custom geometry is often necessary for injection molding, extrusion, packaging, and specialized processing equipment. | Engineering drawing approval process, prototype lead time, previous non-identifying samples, and design-change control procedure. | Medium |
| Testing and Sample Approval | A pre-production sample should be tested at the requested voltage, power, dimensions, and installation conditions before bulk production. | Sample approval identifies fit, wiring, temperature, and control issues before they affect the full order. | Sample test plan, approval form, photographs, test data, and written confirmation of approved specifications. | High |
| Certifications and Compliance | Confirm compliance requirements for the destination market, such as electrical safety, restricted substances, and quality-management systems. | Compliance documentation may be required for import, customer audits, or integration into certified equipment. | Applicable certificates, declarations, audit reports, quality-management certificate, and certificate validity verification. | Medium |
| Lead Time and Production Capacity | Evaluate sample lead time separately from repeat-order lead time; confirm realistic monthly capacity and peak-season arrangements. | Reliable delivery is essential when heaters are maintenance-critical or required for equipment commissioning. | Written production schedule, capacity statement, sample and mass-production lead times, and shipment history with identifying details removed. | Medium |
| Packaging and Export Protection | Packaging should protect ceramic insulation, terminals, and heater geometry from impact, moisture, and compression during transportation. | Ceramic components may be damaged by shock or incorrect stacking even when the outer carton appears intact. | Packaging specification, drop or transport protection method, moisture protection, carton markings, and pre-shipment photographs. | Medium |
| Warranty and Technical Support | The warranty should define coverage, exclusions, operating conditions, installation requirements, and response times for technical issues. | Clear after-sales terms help distinguish manufacturing defects from installation or control-system problems. | Written warranty, troubleshooting guide, installation manual, replacement policy, and technical-support contact process. | High |
| Total Cost of Ownership | Compare purchase price together with energy consumption, replacement frequency, downtime risk, freight, tooling, and spare-parts availability. | A lower initial price may result in higher operating cost or more frequent production interruptions. | Formal quotation, energy and power data, expected service assumptions, spare-parts pricing, freight terms, and replacement lead time. | High |
Choosing the best ceramic insulated band heater in China starts with the machine, not the catalogue. Measure the barrel diameter, heating length, voltage, and available power. Check the target temperature and required watt density. A heater that is too powerful may create hot spots or damage polymer residue. A weaker model may run continuously and waste energy. I learned this after selecting by price alone; the heating time looked acceptable, but temperature recovery was poor.
Ask the manufacturer for dimensional drawings, wiring details, insulation resistance, and test records. Confirm the ceramic blocks fit tightly inside the metal band. Request materials that suit your working temperature and production environment. Clear technical communication matters, especially when metric dimensions and custom terminals are involved. Keep written specifications.
Installation should begin with a clean, dry barrel surface. Remove old material carefully. Do not force the band around an incorrect diameter. Tighten the clamps evenly, leaving no visible gap. Connect grounded wiring through suitable protection, and place the temperature sensor firmly against the controlled zone. Loose sensors can produce unstable readings. Allow gradual heat-up during the first cycle.
Maintenance is simple, but often neglected. Inspect terminals for discoloration, check cable insulation, and remove accumulated plastic before it hardens. Measure resistance during scheduled shutdowns. Replace damaged ceramic sections promptly. Keep a record of operating temperature and failures. My earlier maintenance notes were too vague, so they were nearly useless. A practical checklist would have prevented that mistake.
1901 West Main Street
Washington, MO 63090
Main Directory: 1-800-227-4873
Email: sale@pangcofurniture.com

We’re always looking for talented individuals to join our team. Send us your resume using the form below. When a position comes available that matches your skillset, one of our team members will reach out to you.
"*" indicates required fields